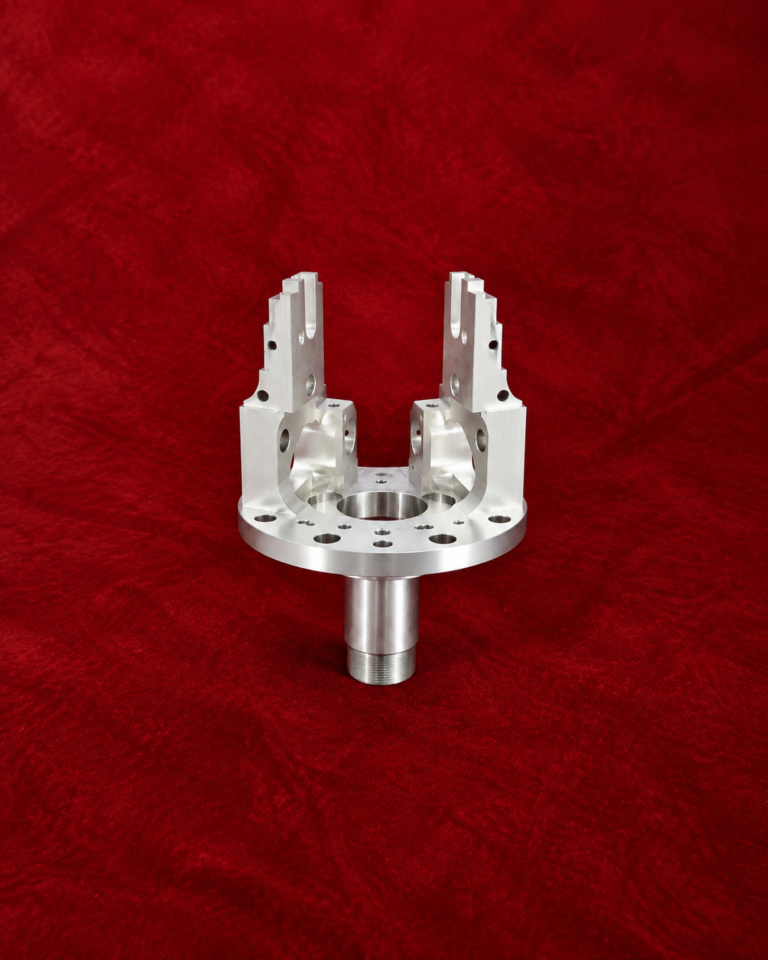
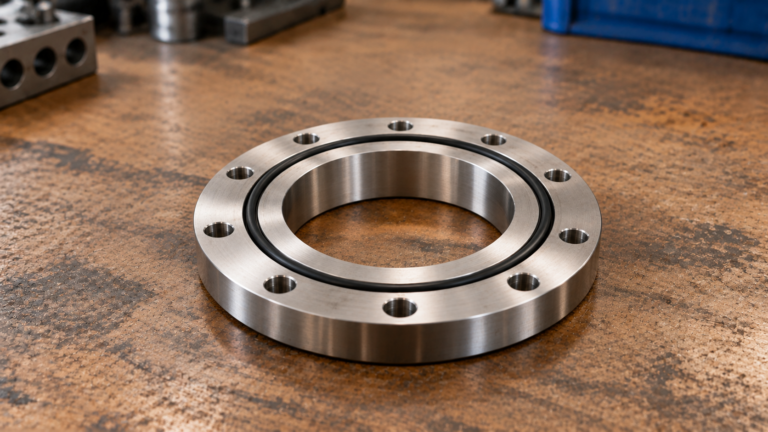
CNC milling surface finish Ra 3.2 μm
Guide to Selecting CNC Surface Roughness (Ra)
Ra Unit: μm (micrometers); indicated on drawings as “Ra X.X”. The lower the number, the smoother the surface, but the higher the machining cost and the longer the processing time.
Core Logic: Select based on part function and assembly requirements; do not blindly choose high surface finish specifications.
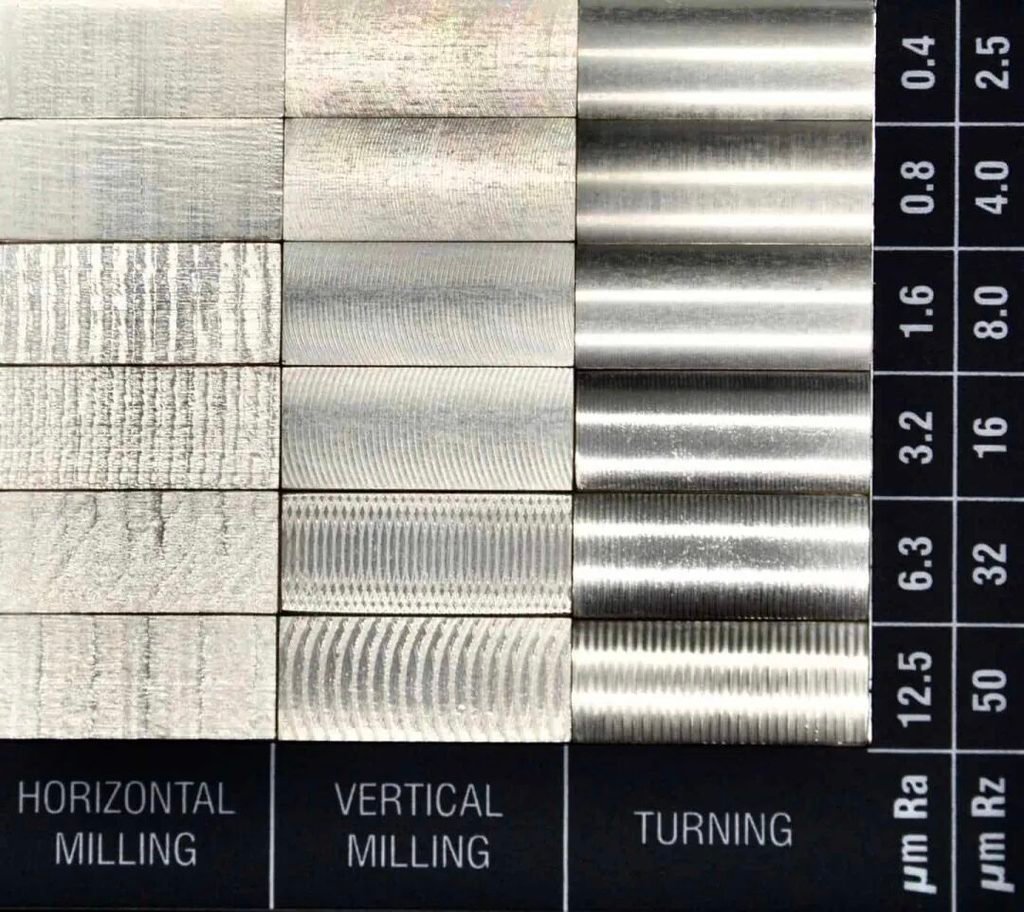
I. Common Ra Grades: Machining Methods, Applications, and References
Ra (μm) | Appearance/Feel | Machining Method | Application Scenario | Notes
Ra 50 | Visible tool marks, rough | Rough turning/milling, stock removal | Non-mating free surfaces, raw castings, non-contact exterior surfaces | Usually no assembly; removes excess material only
Ra 25 | Distinct tool marks | Rough machining | Base bottoms, non-mounting support surfaces | Not recommended for mating surfaces
Ra 12.5 | Visible tool marks, textured to the touch | Semi-finish turning/milling | Non-mating contact surfaces, housings/casings, non-critical locating surfaces | Most common standard machining (e.g., UG roughing + semi-finishing)
Ra 6.3 | Slight tool marks, feels mostly smooth | Finish turning/milling | General locating surfaces, bolt mounting surfaces, standard spigots, non-mating bearing housing surfaces | ✅ Most common in workshops; best cost-performance ratio
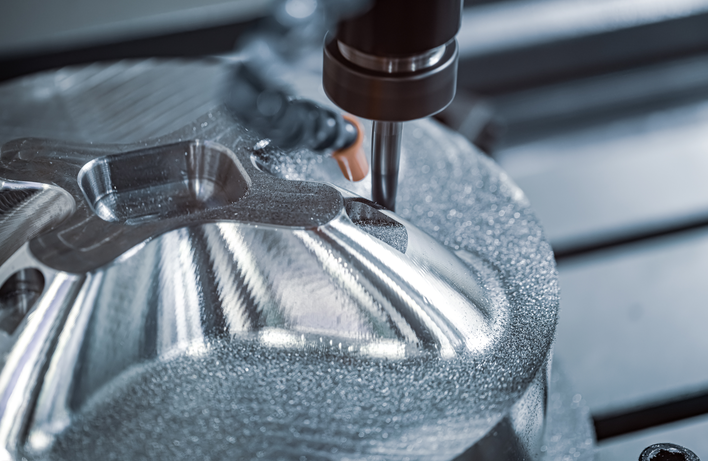
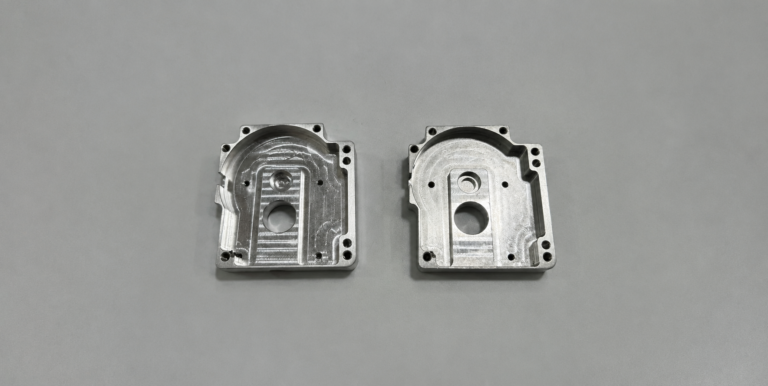
Ra 3.2 | Tool marks barely visible | Finish turning/milling (optimized feed & tool nose radius) | Standard mating surfaces, pin holes, standard shaft ODs, static seal surfaces | Widely used for shafts and housings; achievable via standard CNC finishing programs
Ra 1.6 | Mirror-like finish, no visible tool marks | Precision boring/turning (low feed + large tool nose radius), reaming | Sliding mating surfaces, oil seal seats, pistons, precision locating surfaces | Requires controlled feed/speed and high-quality tooling; costs increase
Ra 0.8 | Mirror finish | Grinding, honing, polishing, precision grinding | Precision bearing bores, hydraulic sealing surfaces, precision sliding pairs | Difficult to achieve consistently via direct CNC milling/turning; usually requires subsequent grinding
Ra 0.4 & below | High-gloss mirror finish | Grinding/polishing | Measuring tools, mold cavities, ultra-precision parts Cannot be achieved by CNC machining alone; post-processing is required.

II. Recommended specifications for different part features (Key Points)
- Threads (Commonly machined)
- Standard fastening threads (M8–M30): Ra 6.3–12.5; Ra 12.5 on the thread flank is perfectly adequate.
- Precision transmission threads: Ra 3.2.
Note: Specifying Ra 1.6 for threads is not recommended; it is difficult to machine and unnecessary.
- Holes
- Drilled holes (rough): Ra 12.5–25
- Precision bored holes: Ra 3.2–6.3
- Reamed holes: Ra 1.6–3.2 (preferred for dowel pin mating holes)
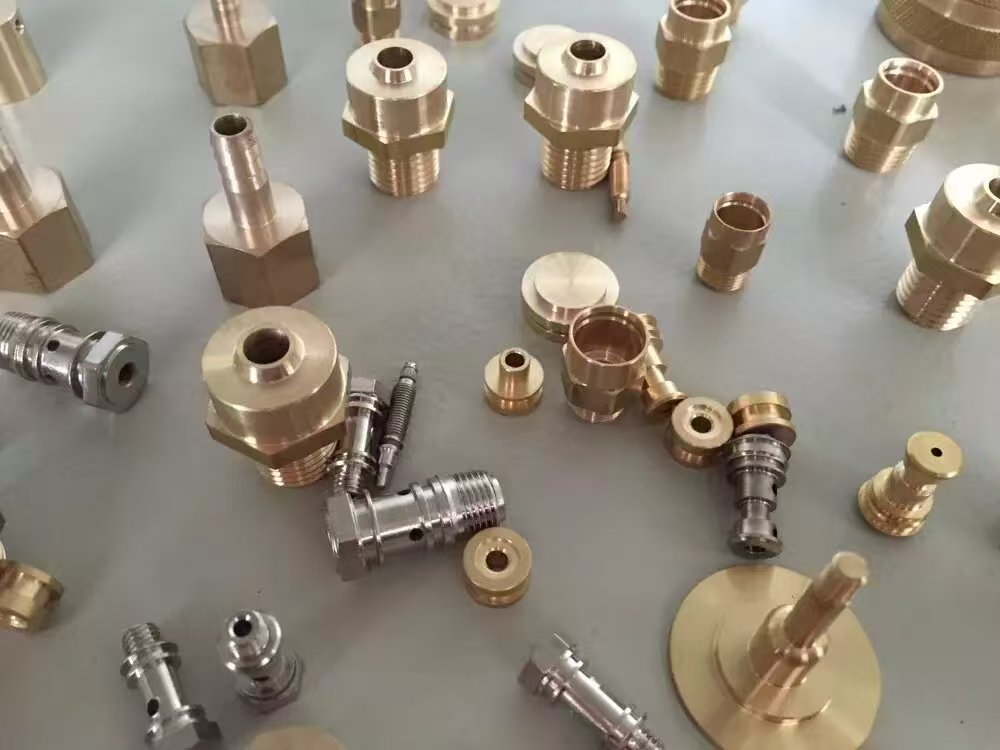
- Shaft outer diameters
- General assembly surfaces: Ra 6.3
- Sliding surfaces for oil seals/O-rings: Ra 1.6 (oil seals require this grade to prevent leakage)
- Bearing mounting surfaces: Ra 1.6
- Flat surfaces
- Bolt seating surfaces: Ra 6.3
- Locating datum surfaces: Ra 3.2–6.3
- Sealing contact surfaces: Ra 1.6–3.2
- Non-mating cosmetic surfaces
Housings, decorative surfaces, and parts with no assembly requirements: Ra 12.5 is sufficient (cost-effective).