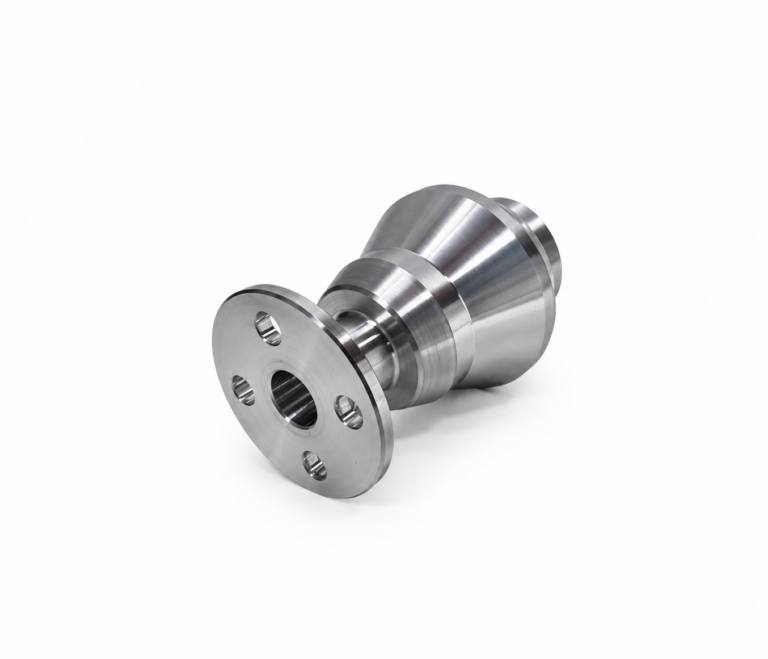
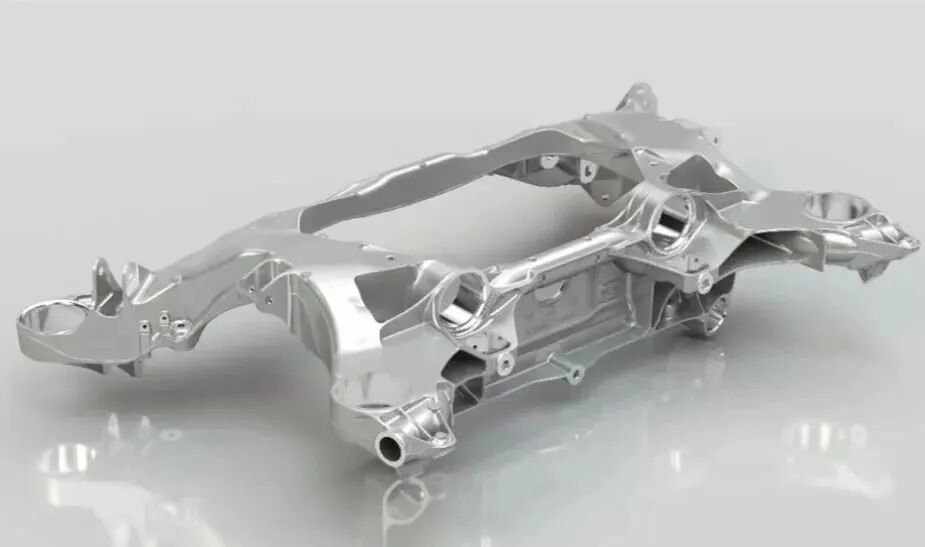
CNC machined aluminum automotive brackets
Guide to Custom Machined Parts: How to Source Truly Reliable Precision Components
I. What Are Custom Machined Parts?
Custom machined parts are components created by removing excess material from a solid block of raw material using CNC machine tools (most commonly CNC milling and CNC turning). Unlike casting, forging, or 3D printing, machining is a subtractive manufacturing process: the machine tool continuously removes excess material until the final geometry is achieved.
The “custom” aspect means that every feature of the part—dimensions, tolerances, threads, hole locations, surface finish, and material grade—is determined by your engineering drawings and CAD models, rather than by a supplier’s standardized product catalog. Custom machined parts are used across virtually every industry:
Medical Devices — Instrument housings, implant-grade components, surgical tools
Aerospace & Defense — Structural brackets, engine components, precision tooling
Automotive — Transmission parts, sensor housings, custom jigs and gauges
Industrial Automation — Robotic arms, custom pulleys, mounting plates, end-effectors
Electronics — Heat sinks, chassis components, connector housings
Consumer Products — Prototypes, enclosures, decorative metal parts
II. Why Are Custom Machined Parts Superior to Standard Parts?
Standard parts are certainly economical—until they fail to meet your specific needs. Custom machined parts offer advantages over standard parts in four key areas:
- Precise Fit and Functionality. Parts are specifically designed around your assembly structure, load requirements, and operating environment, eliminating costly rework, shim adjustments, and field modifications.
- Freedom of material choice. You can select the exact material grade—ranging from lightweight 6061-T6 aluminum alloy to corrosion-resistant 17-4 PH stainless steel.
- True Precision. Modern CNC machine tools can typically achieve stable tolerances of ±0.025 mm (approx. ±0.001 inch), with high-precision machining reaching ±0.005 mm. This level of repeatability is precisely what eliminates the need for manual fitting during assembly.
- Seamless mass production. The same CAM program and tooling setup can be used to transition from a single prototype to full-scale production; the validated process becomes the final production process.
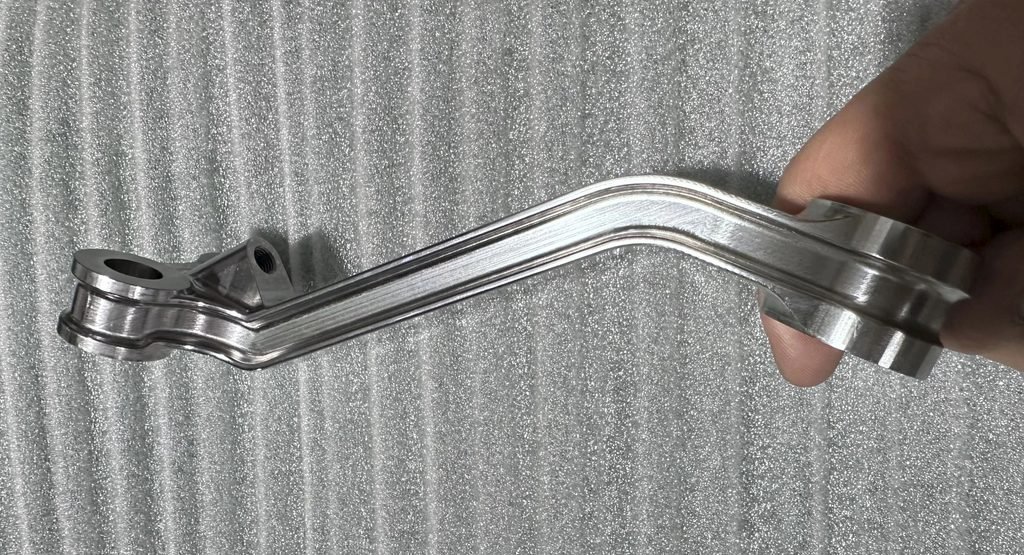
III. Key Manufacturing Processes for Custom Machined Parts
Understanding core processes helps you make the right technical choices—and often, the right choice regarding price.

Most suppliers combine multiple processes within a single workflow: turning for the main body, milling for specific features, and finishing with grinding or surface treatment. A single machining center can often deliver a complete part without secondary operations, thereby shortening lead times and minimizing cumulative tolerance errors.
IV. How to Select Materials for Custom Machined Parts?
Material selection accounts for roughly one-third of the cost of custom machined parts and determines the majority of their performance characteristics. Base your choice on service conditions rather than just the price per kilogram.

Before finalizing the material, confirm three points with the supplier: Can the specific grade be machined effectively to the required tolerances? Can it withstand the operating temperatures and chemical environment? Do surface finish requirements necessitate post-processing steps like anodizing or passivation?
V. Tolerances and Surface Finish: Understanding the Language of Precision
Tolerances are the most frequently misunderstood specifications in custom machining. Tighter is not always better—each order-of-magnitude increase in precision entails more machining time, additional inspection steps, and higher costs.
Standard tolerance: ±0.1 mm — Suitable for most structural and cosmetic parts
Precision tolerance: ±0.025 mm — Typically used for mating surfaces and interference fits
High-precision tolerance: ±0.005 mm — Reserved for critical features such as bearing seats and optical mounts
The same logic applies to surface finish. A surface roughness of Ra 3.2 µm is generally sufficient for most machined parts; bearing surfaces may require Ra 0.8 µm, while sealing surfaces might demand Ra 0.4 µm or finer—levels typically achieved through grinding or polishing.
A practical rule of thumb: specify tight tolerances and fine surface finishes only for features where they are functionally essential, while maintaining standard default values for the rest. This approach significantly reduces costs and lead times without compromising performance.